
INDUSTRY
Pharmaceutical Industrial
Automation Solutions
Pharmaceutical manufacturing environments require reliable process control, accurate data, traceability, and consistent production performance to support quality, compliance, and operational efficiency. INTEG delivers industrial automation and system integration solutions for the pharmaceutical industry through PLC, SCADA, HMI, MES, reporting, historian, batch control, and process control systems.
Whether managing production lines, clean utilities, batching processes, environmental monitoring, packaging areas, or plant-wide operations, automation systems help pharmaceutical manufacturers reduce manual intervention, improve visibility, standardise processes, and maintain greater control across critical manufacturing activities.
INTEG’s pharmaceutical automation solutions are designed to support operational reliability, process consistency, improved visibility, and scalable system performance across regulated production environments.
Implementing Automation and Visibility in Pharmaceutical Manufacturing
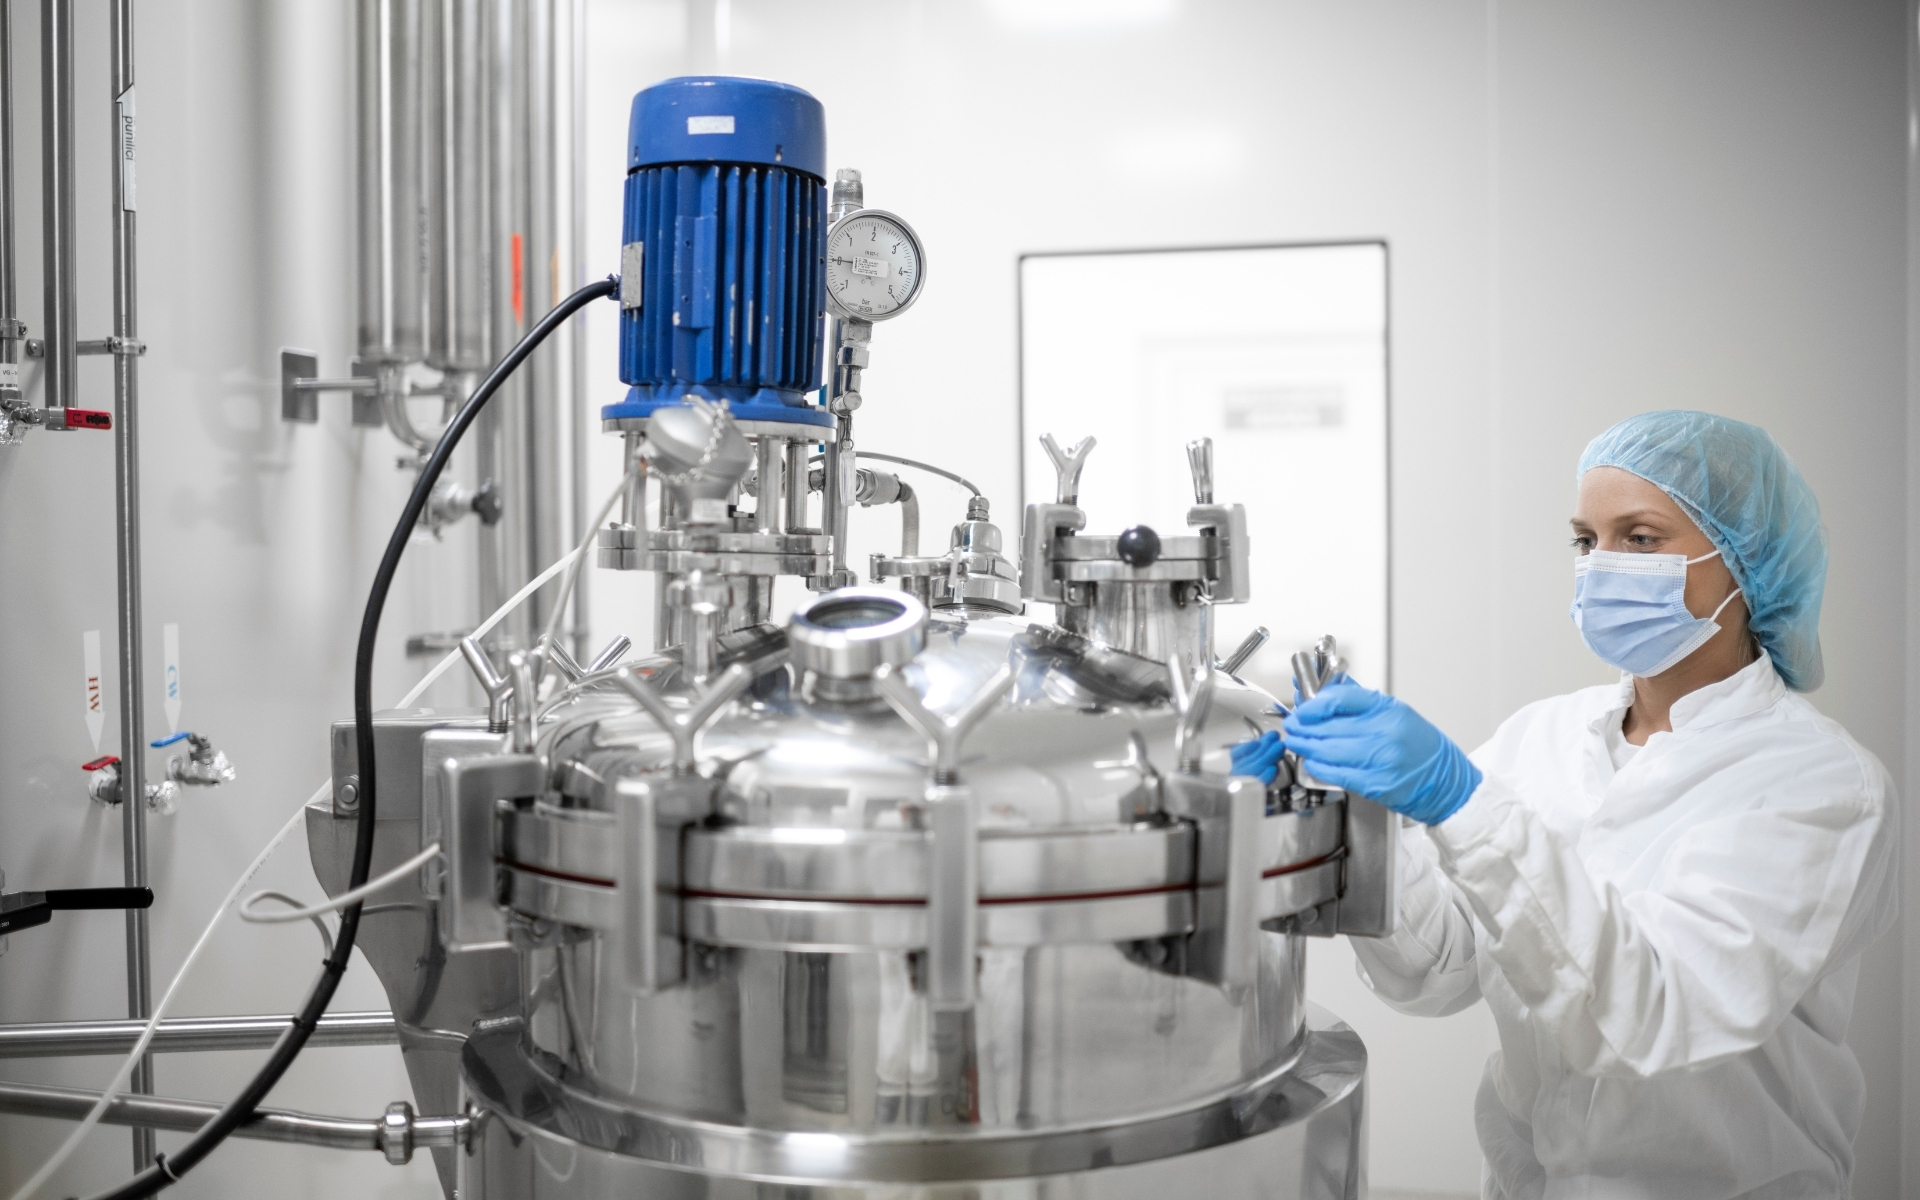
Pharmaceutical operations depend on accurate process control, reliable data, and clear visibility across production environments. Without connected automation and reporting, teams may struggle to monitor process conditions, production performance, alarms, deviations, and critical operational trends.
INTEG helps pharmaceutical manufacturers connect PLC, SCADA, HMI, MES, historian, reporting, and process control systems to improve monitoring, control, traceability, and decision-making.
This supports better production visibility, improved process consistency, faster response to issues, reduced manual reporting, and a scalable automation foundation for long-term manufacturing operations.
Why Food and Beverage Manufacturers Love Working With INTEG
INTEG delivers industrial automation and systems integration solutions designed around real-world manufacturing environments. The focus is not only on implementing technology, but on creating systems that improve reliability, visibility, and long-term operational performance.
Industry Experience
Experience delivering automation projects within food and beverage environments where consistency, hygiene, traceability, and quality are critical operational requirements.
Scalable System Design
Systems are designed to support current operations while allowing future production expansion and additional functionality.
Standards-Based Automation
Implementation approaches align with recognised industrial standards including ISA-88 and ISA-95 methodologies where appropriate.
Plant Wide Visibility
Connected systems provide operators and management teams with real-time information across processes, production lines, and plant operations.
Proven Integration Capability
Experience integrating PLCs, SCADA platforms, MES systems, historians, batching platforms, instrumentation, and plant-level systems.
Why Pharmaceutical Manufacturers Love Working With INTEG
INTEG delivers industrial automation and systems integration solutions designed around real-world manufacturing environments. The focus is not only on implementing technology, but on creating systems that improve reliability, visibility, consistency, and long-term operational performance.
Regulated Manufacturing Experience
Experience delivering automation solutions for manufacturing environments where consistency, process control, traceability, data accuracy, and quality requirements are critical to daily operations.
Reliable Process Control
Control systems are designed to help pharmaceutical manufacturers manage production processes consistently across equipment, systems, and operational areas.
Plant-Wide Visibility
Connected systems provide operators, engineers, quality teams, and management with real-time information across production processes, utilities, equipment, and plant operations.
Data Collection and Reporting
Historian and reporting systems help manufacturers capture operational data, review trends, monitor performance, and support better production and quality-related decision-making.
Scalable System Design
Systems are designed to support current operational requirements while allowing for future expansion, additional functionality, and integration with plant-level systems.

Proven Integration Capability
Experience integrating PLCs, SCADA platforms, HMIs, MES systems, historians, instrumentation, reporting tools, and process control systems into practical automation solutions.
Ready to Plan Your Next Automation Project?
FREQUENTLY ASKED QUESTIONS
Pharmaceutical Industrial Automation
Industrial automation in pharmaceutical manufacturing refers to using technologies such as PLCs, SCADA systems, HMIs, MES platforms, sensors, instrumentation, and reporting systems to monitor, control, and improve manufacturing operations.
SCADA gives pharmaceutical manufacturers real-time visibility and control across critical production systems. It helps teams monitor equipment, alarms, process conditions, utilities, and plant performance from a centralised interface.
Automation improves process consistency, reduces manual intervention, increases operational visibility, supports better data collection, improves response times, and helps teams maintain greater control over production activities.
Yes. Existing pharmaceutical control systems and production environments can often be upgraded through modernising PLC upgrades, SCADA improvements, MES integration, historian systems, instrumentation, reporting tools, and system integration without replacing the entire system.